585.204.6770
sale@sanblueplastics.com
Your Source for Trays!
Choosing a reliable Barbed Wire Making Machine manufacturer requires more than comparing prices and catalog photographs. In 2026, buyers should examine production capacity, machine stability, technical support, and documented quality procedures. A dependable manufacturer explains wire diameter ranges, line speed, material compatibility, and power requirements clearly. It should also provide practical evidence, such as factory videos, installation records, test reports, and customer references.
Small details matter. Inspect the wire-feeding system, twisting accuracy, cutting performance, and tension control. Ask how the machine performs during continuous operation, not only during a short demonstration. Experienced suppliers can discuss maintenance intervals, replacement parts, operator training, and troubleshooting procedures without vague promises. Their engineers should understand galvanized wire, high-tensile wire, and common production adjustments.
Not every ranking is fully objective. Some manufacturers publish limited technical data, while others rely heavily on marketing language. That gap deserves attention. A careful evaluation should compare verified specifications, after-sales responsiveness, warranty terms, and the manufacturer’s export experience. Site visits or live video inspections can reveal workshop organization, testing practices, and actual assembly quality.
Performance comes first.
The best choice may not be the cheapest machine. It should match your planned output, workforce skills, workshop conditions, and long-term maintenance budget. This guide reviews leading Barbed Wire Making Machine manufacturers through a practical and evidence-based lens. It also recognizes that supplier performance can vary by region, model, and service team. Readers should confirm current information before making a final purchasing decision.
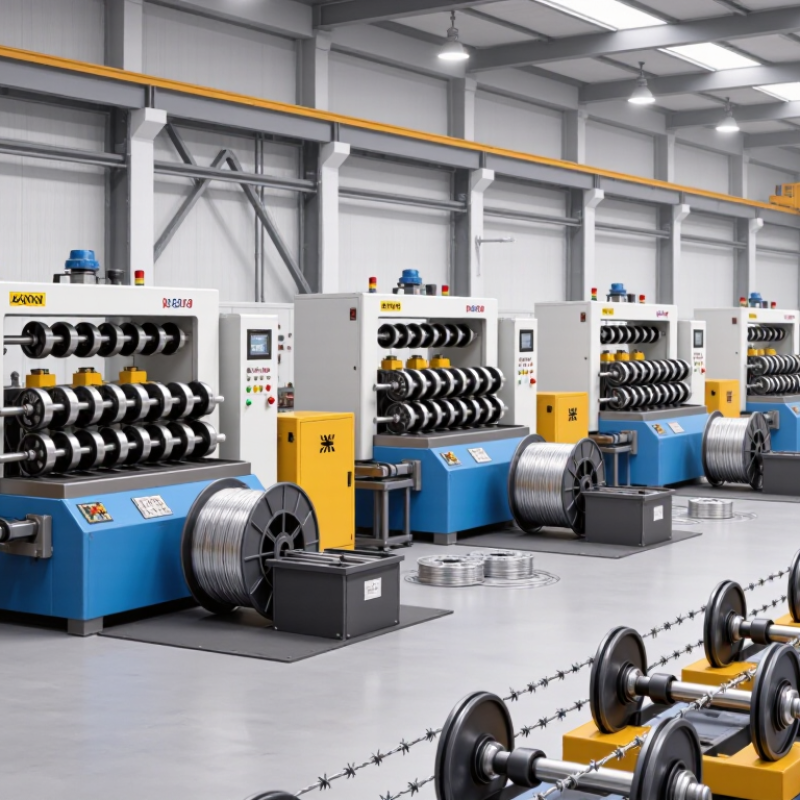
A barbed wire making machine converts smooth steel wire into a continuous fencing product. It usually performs wire feeding, straightening, twisting, barb forming, cutting, and coiling. Some machines use separate wires for the line wire and barbs. Others combine these operations in one production line.
The machine’s core unit is the twisting and barb-forming mechanism. Hardened dies shape each barb at fixed intervals, while rotating spindles wrap the barb wire around the line wire. Operators typically adjust wire diameter, barb spacing, twisting speed, and coil length. ASTM A121 provides widely used specifications for zinc-coated steel barbed wire, including coating and dimensional requirements. Quality control should check tensile strength, barb symmetry, spacing, and coating adhesion.
Industry demand supports continued equipment investment. Grand View Research reported that the global fencing market was valued at about USD 30 billion in 2023, with steady growth projected through 2030. A 2024 industrial machinery analysis also identified automation and lower labor dependence as major purchasing factors. These figures do not measure barbed wire machines directly, so applying them to machine demand requires caution. The assumption may be too broad.
In practical production, uneven wire tension causes loose twists and misplaced barbs. Excessive speed can worsen the defect. A reliable machine therefore needs tension sensors, guarded moving parts, emergency stops, and accessible adjustment points. In my view, output speed matters, but stable geometry matters more. A fast machine producing inconsistent coils is not efficient.
Manufacturer-neutral technical reference table for evaluating commercial barbed wire making machines
| Data Dimension | Typical Commercial Specification | Technical Description and Buying Consideration |
|---|---|---|
| Machine Definition | Automatic barbed wire forming equipment | A barbed wire making machine continuously twists one or two line wires and inserts or forms sharp barbs at preset intervals. The finished product is normally collected into coils for fencing and perimeter-security applications. |
| Basic Product Structure | Two-strand line wire with four-point barbs | The most common commercial configuration uses two longitudinal wires with four-point barbs. Two-point and other configurations may be available when the machine is equipped with different barb-forming tooling. |
| Compatible Wire Material | Low-carbon steel wire, galvanized steel wire, or coated steel wire | Machine selection should match the actual surface condition, tensile strength, coating, and diameter of the wire. Galvanized steel is widely used because the zinc coating improves resistance to atmospheric corrosion. |
| Line Wire Diameter | Approximately 1.6–2.5 mm | This is a common working range for general-purpose barbed wire equipment. The exact range depends on the forming dies, twisting system, wire tensile strength, and machine design. |
| Barb Wire Diameter | Approximately 1.6–2.5 mm | The barb wire is usually selected within a similar diameter range to the line wire. The selected diameter must be compatible with the cutting and twisting mechanism to prevent broken barbs or uneven points. |
| Barb Spacing | Commonly 75–150 mm | Barb spacing is normally adjustable through the machine control system or gear arrangement. Typical products include approximately 75 mm, 100 mm, and 150 mm spacing, depending on the target fencing specification. |
| Production Speed | Approximately 20–60 m/min | Actual output speed depends on wire diameter, barb spacing, material quality, machine condition, and operator settings. Higher speed should not reduce barb sharpness, spacing accuracy, or coil consistency. |
| Typical Daily Output | Approximately 1.0–3.0 tonnes per 24 hours | Daily production is affected by operating hours, wire size, coil changes, maintenance stops, and product specifications. A quoted capacity should always identify the wire diameter and barb spacing used for the calculation. |
| Main Drive Motor | Approximately 2.2–5.5 kW | Motor power varies according to machine size, wire diameter, number of twisting units, and automation level. A properly sized motor should provide stable torque without excessive vibration or overheating. |
| Barb Forming Method | Cut-and-twist or integrated forming system | The machine cuts short barb sections or forms barbs from supplied wire and then twists them around the line wires. Tooling quality directly affects point sharpness, barb alignment, and production reliability. |
| Control System | Mechanical control or PLC-based automatic control | Basic machines may use mechanical gears and switches, while automated models can provide adjustable speed, length counting, fault alarms, emergency-stop functions, and easier recipe changes. |
| Finished Coil Weight | Commonly 20–50 kg per coil | Coil weight depends on product diameter, winding equipment, customer handling requirements, and shipping limitations. An automatic take-up unit can improve coil shape and reduce manual handling. |
| Length Measurement | Electronic or mechanical meter counting | A length counter helps maintain consistent coil quantities and supports production records. For accurate sales length, the counting system should be checked periodically against a measured sample. |
| Electrical Supply | Three-phase industrial power; voltage varies by country | Common industrial installations use three-phase power, but the required voltage and frequency must be confirmed before ordering. Electrical components should comply with the installation region and local safety requirements. |
| Safety Equipment | Guards, emergency-stop switches, and protective covers | Rotating shafts, gears, cutting tools, and wire-feed areas should be guarded. Operators should use appropriate eye, hand, and hearing protection and follow lockout procedures during maintenance. |
| Input Wire Preparation | Uniformly wound wire coils with controlled tension | Wire should be free from severe kinks, excessive rust, and inconsistent diameter. A stable pay-off stand and correctly adjusted tension reduce wire breaks and improve barb spacing. |
| Quality Control Points | Wire diameter, barb spacing, barb sharpness, twist tightness, and coil weight | Finished products should be inspected for regular spacing, secure barb attachment, consistent twisting, straightness, surface condition, and accurate coil length or weight. |
| Applicable Product Standards | ASTM A121, ASTM A641, EN 10223-1, or customer specifications | Applicable standards depend on the destination market and product type. ASTM A121 addresses zinc-coated steel barbed wire, ASTM A641 covers zinc-coated carbon steel wire, and EN 10223-1 is used for steel wire fencing products in relevant European applications. |
| Common Applications | Agricultural fencing, boundary fencing, livestock enclosures, and security barriers | Barbed wire is used where a low-cost physical deterrent and boundary marker are required. Product selection should consider corrosion exposure, animal safety, installation method, and local regulations. |
| Key Manufacturer Evaluation Factors | Verified capacity, tooling life, automation, spare parts, and after-sales support | When comparing suppliers, request a production test using the intended wire diameter and spacing. Also verify machine documentation, electrical standards, replacement tooling availability, warranty terms, training, and service response. |
Note: The values shown are typical commercial ranges rather than universal specifications. Final machine performance depends on the machine configuration, wire grade, coating, diameter, barb spacing, operating conditions, and applicable product standard.
Leading barbed wire machine manufacturers in 2026 focus on stable output, precise forming, and practical automation. Their equipment should maintain consistent wire spacing during long production runs. Servo-controlled feeding systems help reduce uneven tension and material waste. Clear digital controls also let operators adjust speed, strand diameter, and twist settings quickly. Small screens can still be difficult to read in dusty workshops.
Machine builders with strong engineering experience usually test equipment under changing temperatures and workloads. They reinforce cutting units, gear assemblies, and wire guides for repeated operation. Quality manufacturers provide detailed installation instructions and accessible maintenance points. Sensors can detect wire breaks, jams, and abnormal tension before damage spreads. That matters during overnight production.
Safety remains a key feature. Guarded moving parts, emergency stops, and clear warning labels support responsible operation. Reliable manufacturers also offer training, spare-part guidance, and responsive technical service. Custom configurations may suit different wire materials, coil sizes, and factory layouts. However, automation does not remove every risk. Operators still need regular inspections and practical training. A polished specification sheet can hide inconvenient maintenance tasks. Buyers should request sample output, service records, and realistic production data before choosing a machine.
Top Barbed Wire Making Machine Manufacturers to Consider in 2026 should be assessed through measurable production evidence, not attractive catalog claims.
Research and Markets estimates that the global barbed wire market will expand steadily through 2032, supported by agricultural fencing, infrastructure projects, and perimeter protection. Grand View Research also reports continued growth in the broader fencing market, with automation improving output consistency and labor efficiency.
Experienced buyers should inspect machines during a real production run.
Watch the wire tension, twist uniformity, barb spacing, and coil formation. A reliable manufacturer should provide tested output data, not only speed figures. Modern machines commonly support galvanized or coated wire, adjustable barb intervals, and automatic cutting systems. These features reduce manual handling and material waste.
Energy consumption matters more than many brochures admit. A machine producing faster may still cost more per finished coil. Ask for kilowatt-hour data, maintenance intervals, spare-part availability, and operator training records. CE or equivalent conformity documentation should be verified for the target market.
Factory acceptance testing is useful, but it can be too short. Request sample production using your own wire diameter and coating specification. Reports often show optimistic efficiency assumptions. Real workshops are dustier, noisier, and less predictable. That gap deserves attention in 2026.
Comparing barbed wire machine suppliers requires more than checking advertised speed. Start with the wire diameter range, barb spacing, coil weight, and expected daily output. A reliable machine should produce evenly twisted strands, sharp barbs, and stable tension across long production runs. Ask for sample coils made with your own wire. Photos are not enough.
Examine the forming system, motor controls, steel structure, and guarding around moving parts. Servo control may improve consistency, while simpler systems can reduce maintenance costs. Request power consumption data and a complete list of wearing components. Ask how quickly replacement parts can arrive. Supplier experience matters, but documented testing matters more. Factory videos can look impressive. They can also hide interruptions. Request production records, installation details, and references from similar operations.
Tips: Compare total ownership cost, not only the purchase price. Check training, commissioning, warranty terms, and remote support. Confirm whether operators can adjust barb distance without lengthy downtime. Test emergency stops and access doors before acceptance. A small trial may reveal feeding problems. Leave room for doubt; planned capacity is often higher than real capacity. Also inspect the workshop floor, noise level, cable routing, and finished coil handling. These details affect output every day.
Barbed wire manufacturing is becoming more precise, connected, and energy conscious. In 2026, leading machine manufacturers are focusing on servo-driven twisting systems and automated tension control. These features help maintain consistent barb spacing during long production runs. A practical test involves measuring wire diameter, twist length, and finished coil weight at regular intervals.
Energy efficiency is also changing equipment design. Newer lines use efficient motors, standby modes, and improved transmission systems. These changes can reduce unnecessary power consumption without slowing output. Recycled steel is gaining attention, but its variable surface quality may challenge older machines. Operators must adjust drawing pressure and lubrication carefully. Small errors become visible quickly.
Digital monitoring is becoming more useful, though it is not perfect. Sensors can detect broken wires, uneven feeding, and abnormal vibration before major downtime occurs. However, a dashboard cannot replace an experienced technician. Manufacturers with strong engineering records provide installation training, maintenance schedules, spare-part guidance, and clear performance data. Traceable factory testing matters. So does after-sales response.
Modular machine layouts are another important trend. They allow producers to change wire sizes or add inspection units with less disruption. Safety guards, emergency stops, and easier cleaning access are receiving greater attention. Some equipment still looks impressive but performs poorly under continuous load. Careful buyers should request production trials, sample coils, noise measurements, and documented maintenance intervals before selecting a supplier.