585.204.6770
sale@sanblueplastics.com
Your Source for Trays!
Finding China’s top Custom Steel Plate manufacturer requires more than comparing prices or polished websites. Buyers need evidence of production experience, material control, and dependable communication. A credible supplier should explain its steel grades, thickness ranges, cutting methods, heat treatment, and inspection process clearly.
Details matter. A reliable manufacturer can provide mill test certificates, dimensional reports, chemical analysis, and traceability records for each order. Its workshop may include CNC cutting tables, calibrated testing equipment, and protected storage areas. These practical signs reveal whether the company can manage demanding projects consistently. They also help engineers select suitable plates for bridges, pressure equipment, machinery, shipbuilding, and structural applications.
Quality is never proven by claims alone. It depends on documented procedures, qualified technicians, and inspections completed before shipment. The best supplier should discuss applicable standards, including ASTM, EN, or GB requirements, according to the project location. It should also confirm tolerances, surface conditions, edge preparation, packaging, and delivery schedules in writing.
No supplier is perfect. Delays can occur, specifications may be misunderstood, and minor corrections sometimes become necessary. Honest manufacturers acknowledge these risks and maintain responsive after-sales support. They ask useful questions before production instead of accepting incomplete drawings. This article examines the practical qualities that define a leading Chinese Custom Steel Plate manufacturer. It focuses on production capability, technical credibility, inspection discipline, and customer reliability. The goal is not to praise a company without evidence. It is to help buyers make a careful, informed decision. That approach is safer.
What Defines a Leading Custom Steel Plate Manufacturer in China?
A leading custom steel plate manufacturer begins with process control, not attractive brochures. The World Steel Association reported that China produced about 1,005 million tonnes of crude steel in 2024. This scale creates capacity, but capacity alone does not guarantee dependable plate quality. Experienced manufacturers confirm chemistry, rolling temperature, thickness tolerance, and heat-treatment requirements before production starts.
Traceability is equally important. Each plate should connect to a heat number, test certificate, inspection record, and packing list. Independent testing can verify tensile strength, yield strength, impact toughness, and ultrasonic soundness. Certificates should follow recognized requirements, such as EN 10204 inspection documentation, when specified by the buyer. Reliable suppliers also explain which tolerances they can actually hold. Vague promises create expensive surprises.
Delivery performance reveals operational maturity. A serious factory checks plate flatness after cutting, protects edges during loading, and photographs bundles before shipment. The International Energy Agency has highlighted steel’s continuing importance in infrastructure and industrial investment, increasing pressure for efficient, lower-waste production. Still, no factory gets every variable right. Rolling deviations, port delays, and unclear drawings can cause problems. Honest manufacturers record nonconformities and correct them openly. That practical transparency often matters more than a polished sales claim.
How Custom Steel Plate Manufacturing Works
Custom steel plate manufacturing begins with a practical conversation. Engineers review load, temperature, corrosion exposure, dimensions, and delivery limits. A buyer may request a specific grade, thickness, width, surface finish, or cut shape. That request becomes a production drawing and material specification. Reliable mills verify chemistry through controlled alloy additions and documented heat numbers. Slabs are reheated, rolled, and cooled under monitored conditions. Each stage changes strength, flatness, and internal stress. Small details matter. A plate can look perfect yet fail a tolerance check.
Tips: Share drawings with clear units and tolerance ranges. Confirm whether the project needs normalized, quenched-and-tempered, or as-rolled plate. Ask for mill test certificates, dimensional reports, and traceability records. Inspect sample edges for lamination, burrs, and uneven cutting. Do not accept vague promises. They create expensive rework.
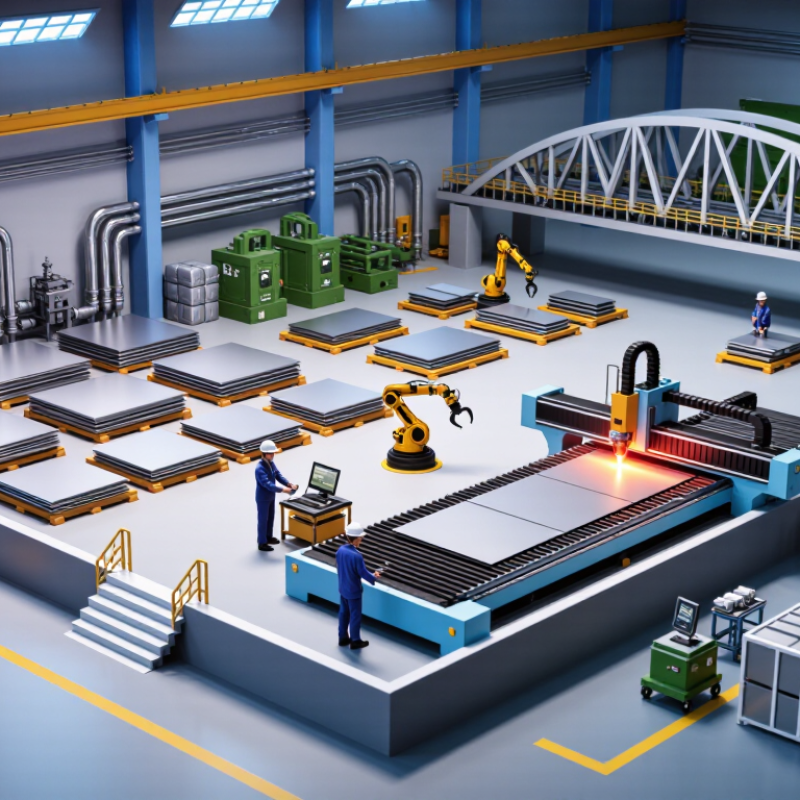
After rolling, plates may receive heat treatment, shot blasting, priming, beveling, drilling, or CNC cutting. Quality teams test hardness, tensile strength, impact performance, and ultrasonic soundness when specified. Independent inspection can add confidence for critical structures. Yet customization is not automatically better. Overly tight tolerances may increase cost without improving service life. In my experience, early communication prevents most avoidable changes. Still, specifications should be challenged when they lack a clear engineering reason. Manufacturing works best when design data, inspection evidence, and actual site conditions agree. They rarely align perfectly.
Choosing a custom steel plate manufacturer requires more than comparing prices. The real question is whether the supplier understands grades, materials, and service conditions. Carbon steel plates suit structural frames and general fabrication. Low-alloy grades offer better strength for demanding loads. Stainless steel helps resist corrosion, heat, and chemical exposure. The correct choice depends on temperature, stress, welding method, and operating environment.
Custom specifications should be written with precision. Include plate length, width, thickness, dimensional tolerance, edge condition, surface finish, and flatness. Grades may follow ASTM, EN, or JIS standards. Heat treatment requirements also matter, especially for quenched and tempered plates. A reliable manufacturer should provide mill certificates, chemical analysis, mechanical test results, and batch traceability. Ultrasonic testing can reveal internal flaws that visual inspection cannot detect.
Details matter most.
From practical fabrication work, a small tolerance error can affect cutting, bending, and assembly. Some suppliers promise every requirement too quickly. That deserves a second look. No specification is perfect on paper. Engineers should review actual loading, welding consumables, and delivery conditions before production. A capable factory confirms unclear points, keeps inspection records, and uses calibrated equipment. It should also protect plates during storage and transport, because rust, impact marks, and moisture can damage acceptable material before installation.
| Steel Plate Category | Common Grade | Applicable Standard | Nominal Yield Strength | Typical Material Composition | Common Applications | Typical Custom Specifications | Available Surface and Delivery Options |
|---|---|---|---|---|---|---|---|
| General Structural Steel | S235JR | EN 10025-2 | Minimum 235 MPa for nominal thickness up to 16 mm | Low-carbon structural steel with manganese and small amounts of silicon; exact limits depend on thickness and product standard. | Frames, brackets, platforms, supports, machinery bases, and general fabrication. | Thickness commonly specified by project drawings; cut-to-size length and width, beveled edges, drilled holes, and welding preparation. | As-rolled or shot-blasted surface; cut lengths, cut-to-shape parts, or full plates subject to order requirements. |
| Higher-Strength Structural Steel | S355JR | EN 10025-2 | Minimum 355 MPa for nominal thickness up to 16 mm | Low-alloy structural steel designed for higher strength than S235 grades; chemical limits are defined by EN 10025-2. | Bridges, building structures, industrial equipment, cranes, trailers, and heavy fabrication. | Custom plate thickness, profiling, edge preparation, tolerance class, ultrasonic testing, and inspection documentation. | As-rolled, normalized, or thermomechanically processed material when specified; standard or project-specific cutting. |
| Pressure Vessel and Boiler Steel | P265GH | EN 10028-2 | Minimum 265 MPa for nominal thickness up to 16 mm | Fine-grain pressure-vessel steel intended for elevated-temperature service; composition and delivery condition are controlled by the standard. | Boilers, heat exchangers, storage vessels, tanks, and process equipment. | Specified thickness, normalized delivery, impact testing when required, ultrasonic examination, forming allowance, and welding-related documentation. | Mill finish or processed surface; supplied as plate, cut blank, or formed component according to fabrication needs. |
| Normalized Fine-Grain Pressure Vessel Steel | 16Mo3 | EN 10028-2 | Minimum 275 MPa for nominal thickness up to 16 mm | Low-alloy pressure-vessel steel containing molybdenum, suitable for elevated-temperature applications. | Boiler components, steam equipment, pressure vessels, and high-temperature process systems. | Heat-treatment condition, impact-test temperature, ultrasonic testing, plate flatness, and machining or profiling requirements. | Normalized delivery is typical; custom cut parts and inspection certificates can be specified. |
| Weathering Steel | S355J2W | EN 10025-5 | Minimum 355 MPa for nominal thickness up to 16 mm | Low-alloy structural steel containing weathering elements such as copper and chromium to promote a protective patina in suitable environments. | Bridges, exterior structures, architectural panels, sculptures, and rail-related structures. | Weathering-grade chemistry, exposed-edge treatment, cut-to-shape panels, surface appearance requirements, and welding procedure compatibility. | As-rolled or blast-cleaned surface; natural patination depends on exposure, drainage, wet-dry cycling, and local atmosphere. |
| High-Yield Structural Steel | S690QL | EN 10025-6 | Minimum 690 MPa for nominal thickness up to 50 mm | Quenched and tempered low-alloy structural steel with high strength and controlled toughness. | Heavy lifting equipment, cranes, transport frames, mining equipment, and weight-sensitive structures. | Quenched-and-tempered condition, low-temperature impact testing, controlled heat input for welding, tight flatness, and precision profiling. | Typically supplied quenched and tempered; machining, drilling, bending, and edge preparation require process control. |
| Shipbuilding Structural Steel | AH36 | ASTM A131/A131M | Minimum 355 MPa | Marine structural steel with controlled carbon, manganese, silicon, and residual elements according to the applicable grade requirements. | Ship hulls, decks, bulkheads, offshore structures, and marine support components. | Marine classification requirements, plate thickness, impact testing, ultrasonic inspection, shot blasting, priming, and profile cutting. | As-rolled or normalized condition depending on grade and approval; marine inspection documentation may be required. |
| Carbon Steel Pressure Vessel Plate | SA516 Grade 70 | ASME SA516/SA516M | Minimum 260 MPa, subject to thickness range and specification requirements | Carbon-manganese steel for moderate and lower-temperature pressure-vessel service. | Storage tanks, pressure vessels, boilers, separators, and petrochemical equipment. | Normalized condition, impact testing, ultrasonic examination, vacuum-box or dimensional requirements, and weld-preparation details. | As-rolled or normalized when specified; supplied with material test reports and optional non-destructive testing. |
| Structural Carbon Steel Plate | ASTM A36 | ASTM A36/A36M | Minimum 250 MPa | Carbon structural steel with requirements for tensile strength, yield strength, elongation, and chemical composition. | General construction, base plates, machine supports, frames, platforms, and fabricated assemblies. | Custom dimensions, plasma or flame cutting, holes, slots, weld bevels, flatness, and dimensional tolerances. | Hot-rolled surface; supplied as full plate, cut plate, or fabricated blank according to drawing requirements. |
| Atmospheric Corrosion-Resistant Steel | ASTM A588 Grade B | ASTM A588/A588M | Minimum 345 MPa | High-strength low-alloy weathering steel with alloying elements that improve atmospheric corrosion resistance under suitable conditions. | Bridges, towers, rail cars, structural supports, and outdoor architectural structures. | Weathering-steel chemistry, thickness and dimensional tolerance, weldability requirements, surface preparation, and cut-part geometry. | Mill finish or prepared surface; corrosion performance depends on the service environment and design details. |
| Stainless Steel Plate | 304/304L | ASTM A240/A240M | Typically 205 MPa minimum for 304 and 170 MPa minimum for 304L, subject to specification | Austenitic stainless steel containing approximately 18% chromium and 8% nickel; 304L has lower carbon content than 304. | Food-processing equipment, chemical equipment, architectural components, tanks, and general corrosion-resistant fabrication. | 2B, No. 1, brushed, or polished finish; laser or waterjet cutting, bending, forming, drilling, and custom surface protection. | Cold-rolled or hot-rolled plate; protective film and edge finishing can be specified for visible surfaces. |
| Stainless Steel Plate | 316/316L | ASTM A240/A240M | Typically 205 MPa minimum for 316 and 170 MPa minimum for 316L, subject to specification | Austenitic stainless steel containing chromium, nickel, and molybdenum; 316L has lower carbon content than 316 and improved weldability. | Marine equipment, pharmaceutical systems, chemical processing, coastal structures, and hygienic applications. | Surface finish, pickling and passivation, weld preparation, dimensional tolerances, cut-outs, forming, and surface protection. | Cold-rolled or hot-rolled; finish selection should match corrosion exposure, cleaning method, and appearance requirements. |
| Wear-Resistant Plate | AR400 | ASTM A tempers or producer-specific wear-grade requirements; verify the purchase specification | Hardness-based grade; nominal hardness is commonly around 360–440 HBW, depending on the applicable specification | Quenched and tempered abrasion-resistant steel with controlled carbon and alloying elements. | Chutes, hoppers, liners, conveyors, mining equipment, crushers, and bulk-material handling systems. | Hardness range, thickness, cut profile, minimum bend radius, hole diameter, bevel geometry, and welding procedure requirements. | Quenched and tempered condition; plasma or waterjet cutting is often preferred for complex profiles and heat-sensitive parts. |
| Boiler and Heat-Exchanger Tube-Plate Material | SA387 Grade 11 | ASME SA387/SA387M | Minimum 310 MPa, subject to grade and thickness | Chromium-molybdenum alloy steel plate designed for welded pressure vessels operating at elevated temperatures. | Heat exchangers, boilers, pressure vessels, refinery equipment, and high-temperature process units. | Normalized and tempered condition, impact testing, ultrasonic inspection, weldability controls, tube-sheet machining, and dimensional tolerances. | Usually supplied normalized and tempered; machining allowance and inspection documentation can be included in the order. |
Quality begins with controlled steelmaking, not a final visual check. For custom steel plates, experienced teams review chemical composition, thickness tolerance, surface condition, and delivery requirements before production. Each heat receives a traceable identification number. That number follows the plate through cutting, testing, inspection, and packing.
Testing must match the plate’s intended service. Optical emission analysis verifies carbon, manganese, and alloying elements. Tensile tests measure strength and elongation. Impact testing can reveal toughness at low temperatures. Ultrasonic testing helps locate internal discontinuities that a clean surface may hide. Inspectors also check flatness, dimensions, edge quality, and visible defects under suitable lighting.
Documentation builds trust. A reliable supplier should provide inspection reports, material certificates, test results, and calibration records. ISO 9001-based quality systems can support consistent control, while EN 10204 3.1 documentation may confirm batch-specific results. Requirements under ASTM, EN, or other applicable standards should be agreed before production, not after shipment. Traceability matters.
No inspection system is perfect. Records expose weak points. A rushed recheck can miss a small defect near a cut edge, so independent verification remains valuable. Equipment must be calibrated, and inspectors need practical training. Honest manufacturers preserve nonconforming samples, review causes, and improve procedures instead of hiding inconvenient results. That discipline gives custom steel plates dependable evidence, not merely attractive paperwork.
Selecting a Chinese custom steel plate manufacturer requires more than comparing quotations. China produced about 1,005 million tonnes of crude steel in 2024, according to World Steel Association data. Large output does not guarantee consistent plate quality. Request mill certificates, chemical analysis, mechanical-test results, and heat-number traceability for every batch. Check whether the supplier can meet your required grade, thickness tolerance, flatness, surface finish, and cutting accuracy.
A serious evaluation includes a remote review and, when practical, an independent factory audit. Inspect plate storage, calibration records, welding procedures, and non-destructive testing controls. Ask for recent production samples, not only showroom photographs. The OECD’s 2024 steel market analysis highlights continuing pressure from excess capacity and weak demand. This makes unusually low pricing worth investigating. Clarify steel origin, processing steps, inspection responsibility, packaging, and delivery terms in the contract.
Small details matter. Can the factory explain a failed tensile test? Can it replace a plate with incorrect dimensions? Ask for production schedules and measurable acceptance criteria. ISO 9001 certification can support process control, but certification alone is not proof of product performance. I would avoid choosing only by price; that shortcut often creates costly rework. No audit is perfect. My own checklist would still include supplier references, third-party inspection, payment protection, and a trial order before larger commitments.